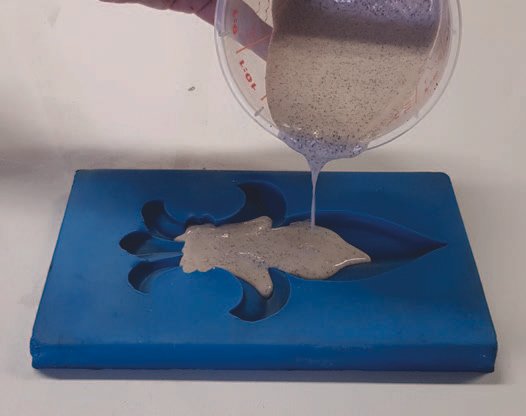
1.0 After mixing, A1 can easily be poured into the mould. Demoulding is often possible after 1 hour. For fragile objects, this may take longer.
If you have not mixed enough A1 for the mould, you can add a new layer of A1 within 1 hour.
2.0 Several techniques can help prevent air bubbles on the surface:
Use the A1 high-shear mixer.
Tap the side of the mould to release any remaining air bubbles.
If possible, start by brushing A1 into the mould so that all uneven areas and relief are covered. The brush marks disappear because the material flows.
Pour the rest of the A1 along the edge so it can flow in smoothly.
If the shape of the mould allows it, fill the mould halfway and rotate it so a thin layer of A1 coats the inside. Pour the remaining A1 back into the cup. Repeat this 3 times before making the final cast. This often works best for bodycasting moulds.
Pour part of the mixed A1 into the mould. If possible, start by brushing the mould so that all uneven areas and relief are covered with A1.
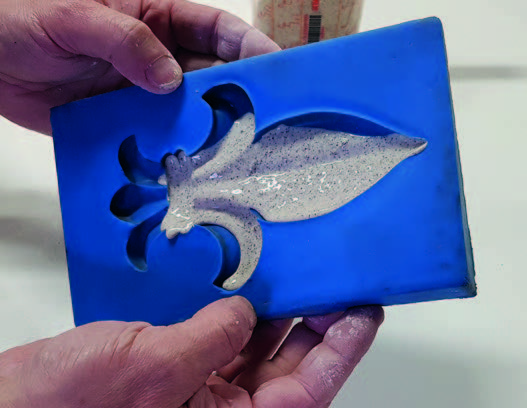
Carefully rotate the A1 in the mould.
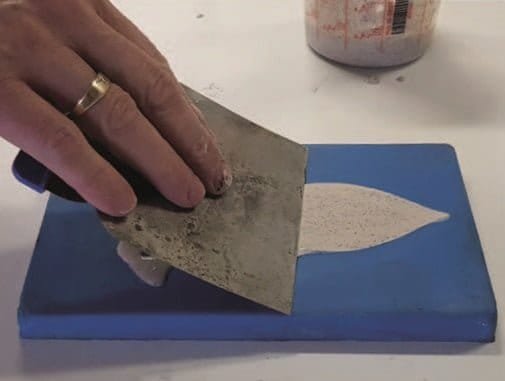
Pour the desired amount of A1 into the mould and scrape off the excess with a putty knife.
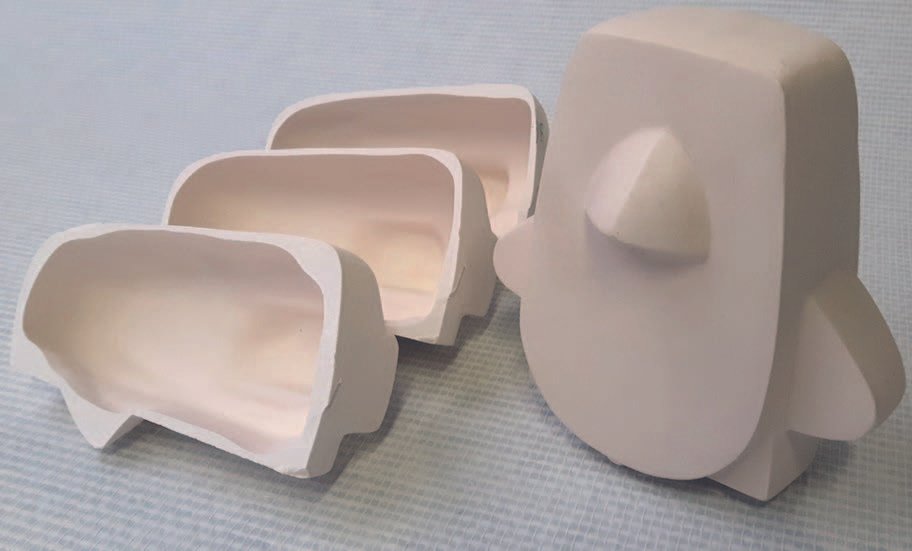
Result after drying and demoulding: a solid cast object, an exact copy of the mould.
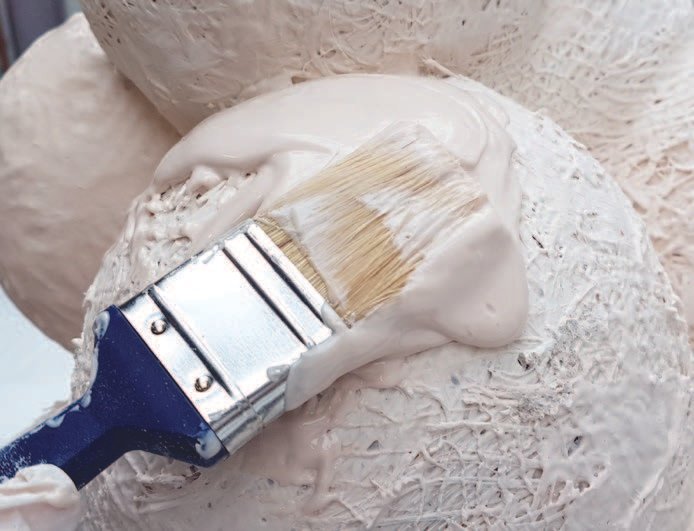
Brush, roller or spatula
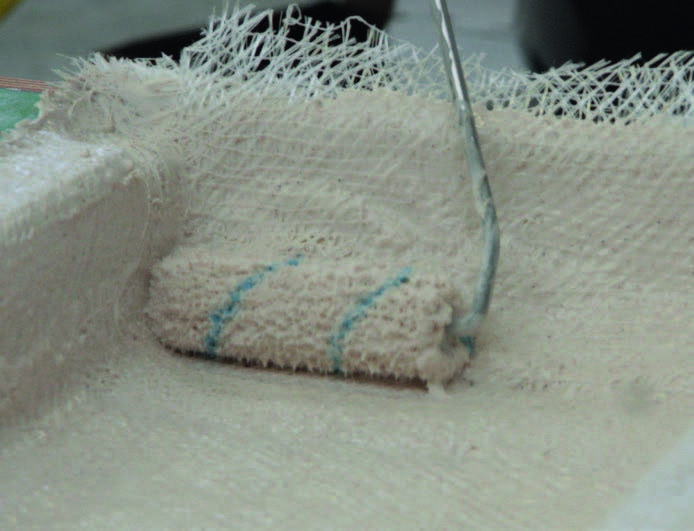
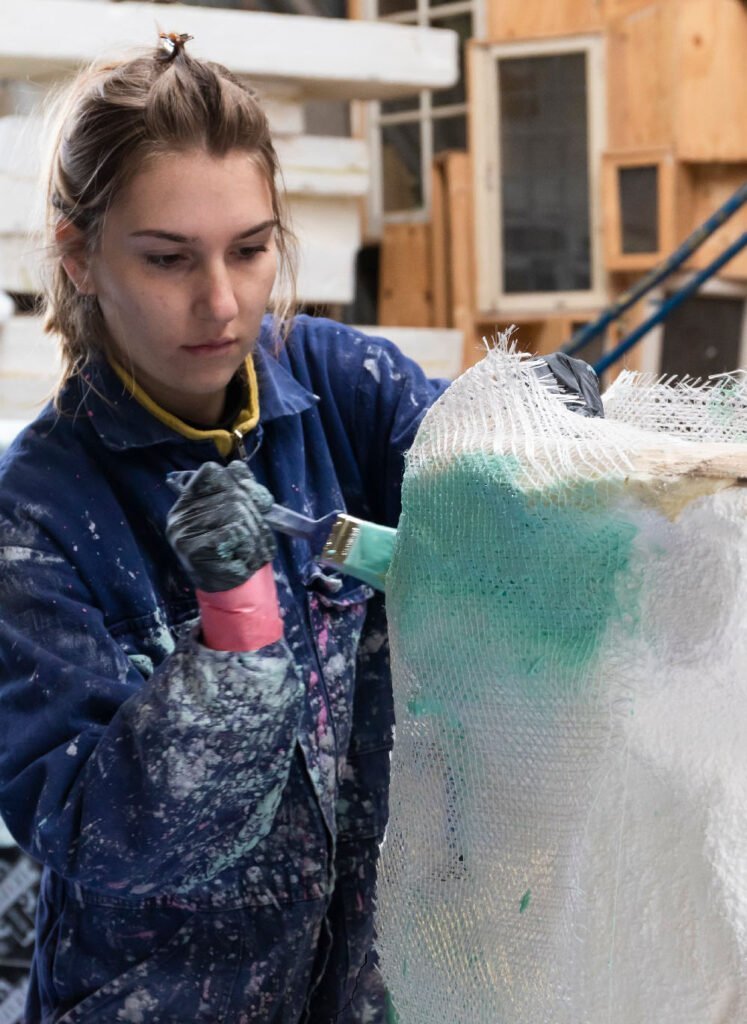
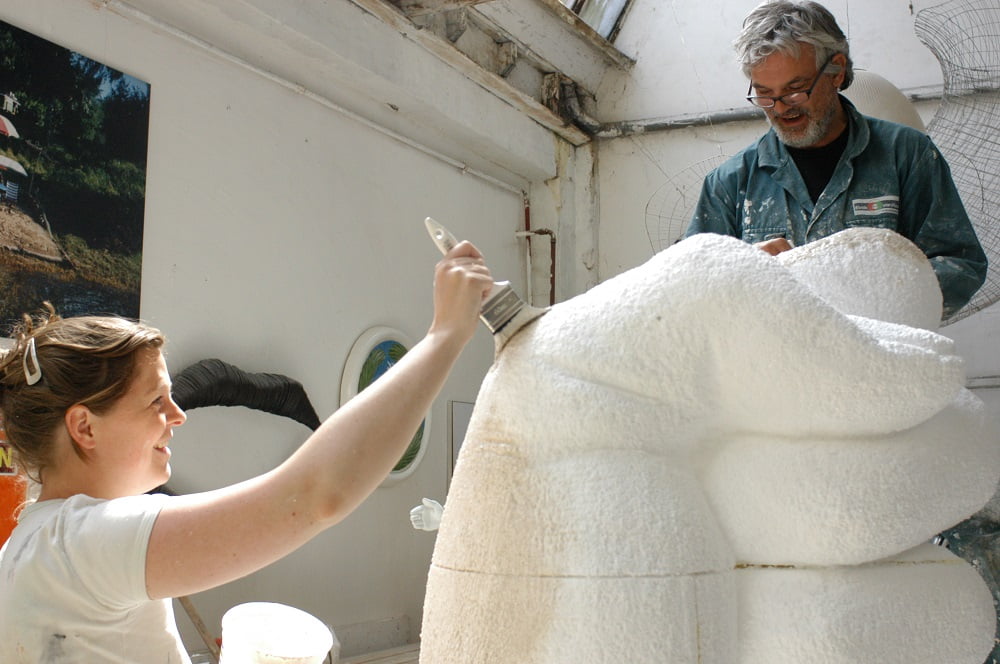
3.0 With a brush or paint roller, A1 can be applied in a thin layer. This is particularly suitable for applying the first layer of A1, the so-called gelcoat layer, or for laminating glass fabric such as A1 Triaxial Fibre.
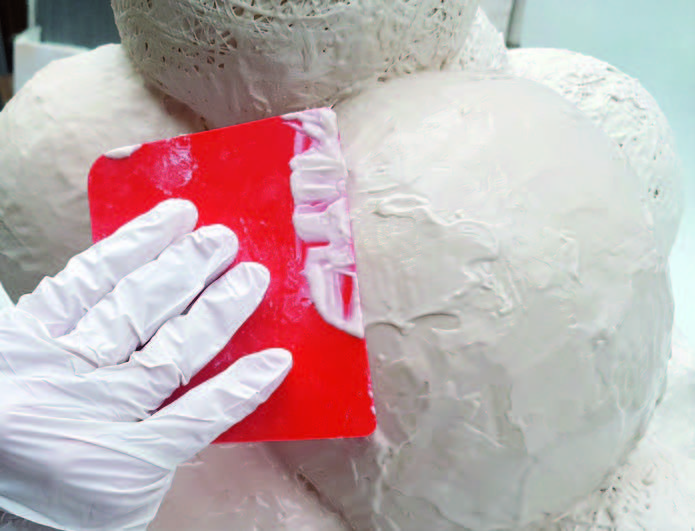
The brush or roller can be cleaned afterwards with water. A spatula is suitable for getting a smooth finish. For this, we advise thickening the A1 with A1 Thix A or A1 ATP Powder.
Brush
Roller
Spatula
Spraying
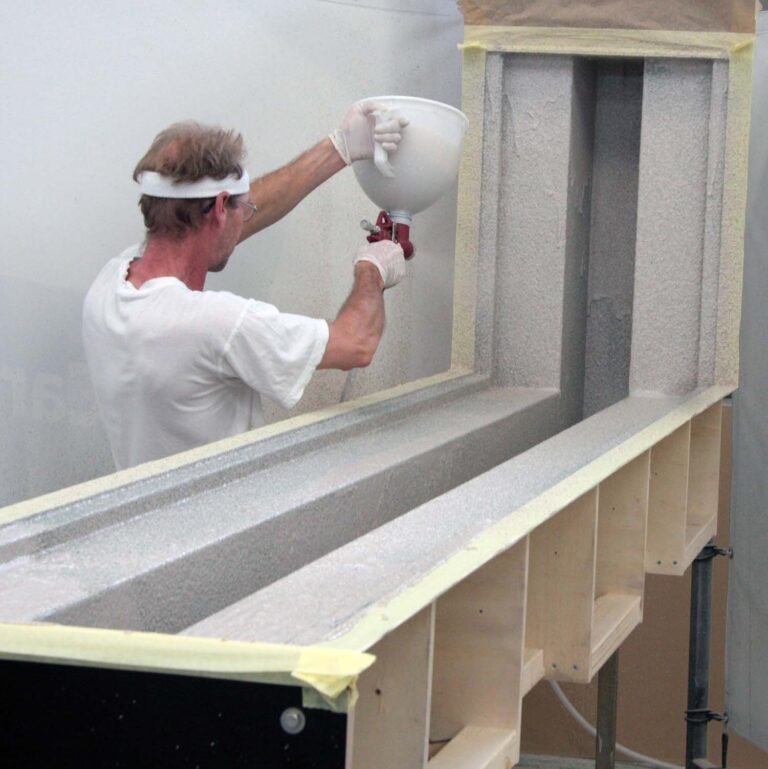
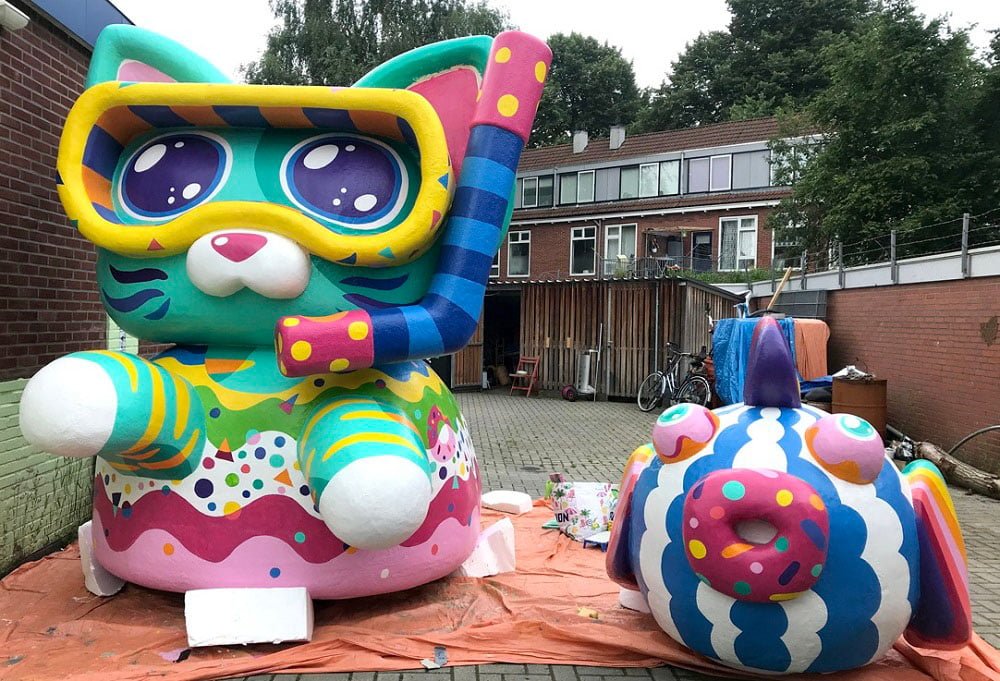
4.0 A1 is easy to spray, which makes it possible to apply a thin layer of A1. This technique is ideal for working with a (silicone) mould, but also for applying A1 to, for example, a form made of EPS (expanded polystyrene).
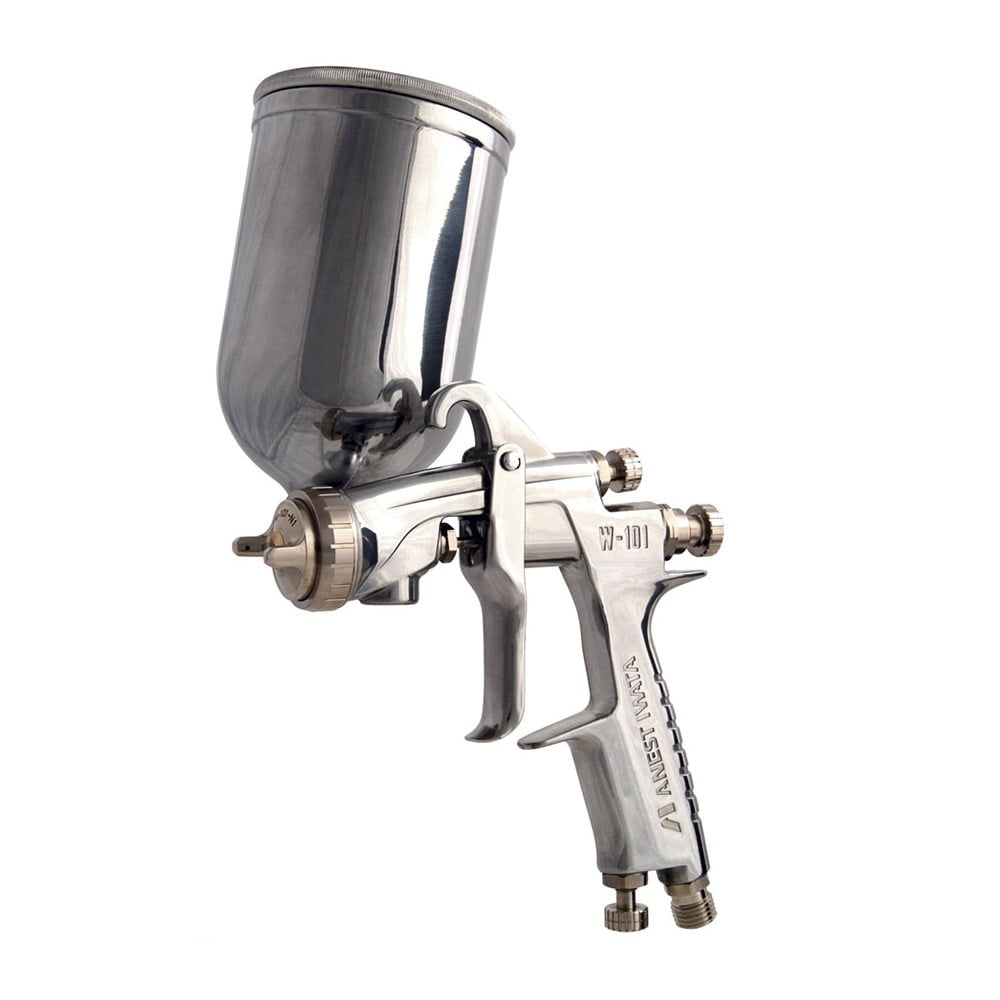
For a cup gun, a minimum nozzle size of 1.5 mm is required. You will get a good result with 2.5 or 3 mm, and even a 3.5 mm nozzle can be used. We suggest sifting the A1 before spraying to remove lumps.
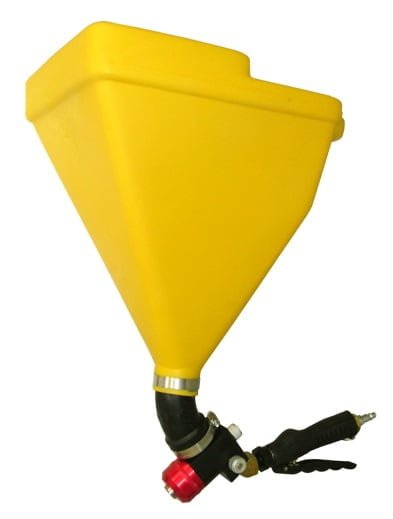
With a hopper gun, the nozzle size can be larger, depending a little on the desired surface quality. Most hopper guns have a nozzle size of 4 to 6 mm. For large quantities, you can also use a large spraying machine with chopped fibres.
Spraying cup
Hopper gun
Rotational moulding
5.0 In a closed (silicone) mould, you can cast not only solid objects but also hollow ones by rotation. For this, we have a special rotation version of A1 (A1 Rotation).
An important advantage of rotational casting is the weight saving, because only a limited amount of A1 is needed compared to solid casting. The result is a lighter, but also more fragile object. In rotational moulding, you pour A1 Rotation into the mould and then rotate it until the entire inner wall of the mould is covered.
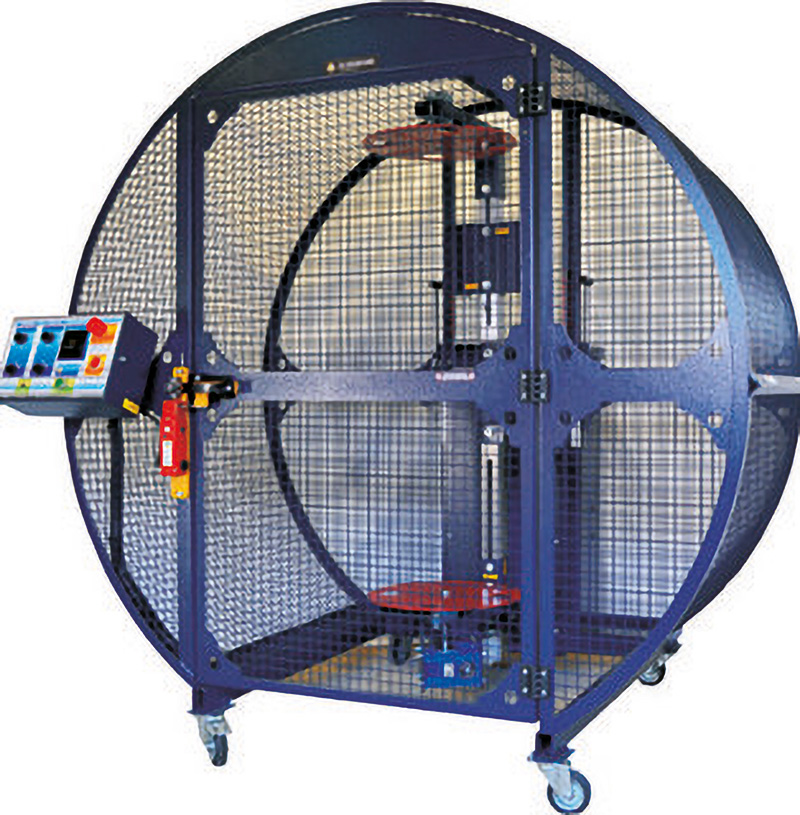
Keep rotating the object until the A1 starts to harden. You can check when it starts curing by looking at the A1 left in the mixing cup. A1 Rotation hardens in around 30 to 40 minutes. The rotation can be done by hand or with a rotating machine. If desired, you can apply a second or even third layer of A1 the same way.
Rotation machine
Phing Thing - Gert-Jan Vlaming
LAMINATING OF AN OBJECT
A1 adheres very well to EPS (expanded polystyrene), which is why this is a frequently used combination. Objects made from, for example, modelling foam can also be covered with A1. To give the object a smooth finish, a layer of A1 mixed with A1 Thix A or A1 ATP Powder can be applied.
6.0 EPS coated with a layer of A1
You can easily apply a layer of A1 to EPS by brushing, spraying, rolling or filling. Sometimes it is necessary to thicken the A1 with A1 Thix A or A1 ATP Powder.
The strength of the A1 top layer also depends on the thickness of the A1 layer and the density of the EPS. For a strong top layer, we recommend using 1 or more layers of A1 Triaxial Fibre.
7.0 EPS coated with a layer of A1, reinforced with A1 Triaxial fibre
Brush the EPS with A1. Press the A1 Triaxial Fibre into the still-wet layer of A1. The A1 Triaxial Fibre gives the A1 its strength. We advise applying at least 2 layers of A1 Triaxial Fibre. Because of the processing time of A1, it helps to cut the A1 Triaxial Fibre to size before you start.
Because you are working over an EPS form, the first layer will be the inner layer and will not be visible later. It is very important that the A1 Triaxial Fibre is completely soaked with A1 in each layer before you apply the next one. Working dry-on-dry traps air and creates weak spots in the object.
8.0 EPS glued with A1 Two pieces of EPS can be glued together using A1. In this case, A1 acts as an adhesive.
Geert Wessels
Studio Maky
9.0 PUR/PIR foam
Although A1 adheres very well to PUR/PIR, we advise against using these foam systems. EPS can do the job with fewer risks. PUR/PIR is easier to shape by hand, but that is probably its only advantage over EPS. EPS has fewer risks, better water resistance and a better price. Thermal expansion is about the same as with EPS, but PUR/PIR has problems with dimensional stability and possible after-foaming caused by moisture. This has to do with the way these systems are produced.
We also strongly advise against filling an A1 product with PUR foam. The chemicals in PUR foam can have a negative effect on A1, and the unpredictable foaming under high pressure can cause cracking, even when using 3 or 4 layers of A1 Triaxial Fibre.
10.0 Sawing and drilling A1
A1 has a processing time of about 20 to 25 minutes. After that, the material is dry but still vulnerable. To saw or drill A1 properly, we advise waiting about a week, when the A1 is (almost) fully cured. Sawing or drilling after 1 day is possible, but be careful, as the A1 object is not yet fully cured. You can use any sawing machine for this, although the result depends on the quality of the machine and the skill of the user. A wet saw table or a Dremel often gives a nice result.
Disclaimer: please be aware for other language translation, some content may not translated properly, you can stay use English language for proper reading
Disclaimer: All (technical) advice and treatment and the possible applications regarding the products are given without obligation, and to the best knowledge and effort, as well as the current state of technology, without an obligation to create results and without any liability. We recommend that the prospective user determines the suitability of our materials and suggestions before adopting them on a commercial scale.